 Authorised Dealer – Murugappa Membranes
Advanced chemical programs for boilers, cooling towers, reverse osmosis systems, and Zero Liquid Discharge (ZLD) plants. Engineered to protect assets, improve heat transfer, and lower total water operating costs.
Advanced boiler water treatment solutions designed for scale control, oxygen scavenging, sludge dispersion, pH control, and condensate corrosion protection across low, medium, and high-pressure steam generators.
| Product Name | Function & Chemistry | Key Benefits |
|---|---|---|
| MaxV® 7075 | Boiler Anti-Scalant | Prevents calcium & magnesium scale formation on heat transfer tubes, improving thermal conductivity. |
| MaxV® 7078 | Polymer-Based Anti-Scalant | Advanced synthetic polymer conditioning that keeps hardness particles fluid for effortless blowdown removal. |
| MaxV® 7079 | Anti-Scalant & Deposit Dispersant | Dual-action dispersant preventing iron and mineral deposits from baking onto heat transfer surfaces. |
| Product Name | Function & Chemistry | Key Benefits |
|---|---|---|
| MaxV® 7071 | Catalyzed Boiler Oxygen Scavenger | Rapidly eliminates dissolved oxygen from boiler feedwater at ambient to moderate temperatures, stopping oxygen pitting corrosion in economizers and feed lines. |
| MaxV® 7072 | Volatile / Non-Sulfite Oxygen Scavenger (DEHA Base) | Zero-solids organic scavenger that volatilizes into steam to protect condensate lines and passivates metal tubes into insoluble protective magnetite (Fe₃O₄). |
| MaxV® 7073 | Tannin Base Oxygen Scavenger | Eco-friendly, 100% organic tannin formulation forming an impervious protective magnetite passivation barrier while conditioning sludge for non-toxic industrial boilers. |
| Product Name | Function & Chemistry | Key Benefits |
|---|---|---|
| MaxV® 7050 | Boiler Feedwater pH Booster | Neutralizes acidic carbonic species in feedwater and establishes strong alkaline buffer (pH 10.5–11.5) for low-to-medium pressure steam boilers. |
| MaxV® 7060 | Boiler pH Booster & Alkaline Builder | High-strength liquid alkaline builder optimizing boiler water alkaline reserve to prevent acidic corrosion attack across drums, headers, and piping. |
| MaxV® 7077 | High-Temp Boiler pH Booster | Thermally stable, high-purity alkaline pH conditioner designed for high-temperature, high-pressure steam boilers preventing caustic gouging and carryover. |
| MaxV® 7065 | Amine-Based Condensate Treatment | Neutralizing and filming volatile amines that carry into steam and protect return condensate lines from carbonic acid attack. |
| MaxV® 3070 | Fire Side Soot Removal | Cleans fire-side tube deposits, catalytic soot breakdown, and enhances fuel combustion efficiency. |
Our boiler treatment range is specifically engineered to control all 7 critical steam-cycle failure vectors:
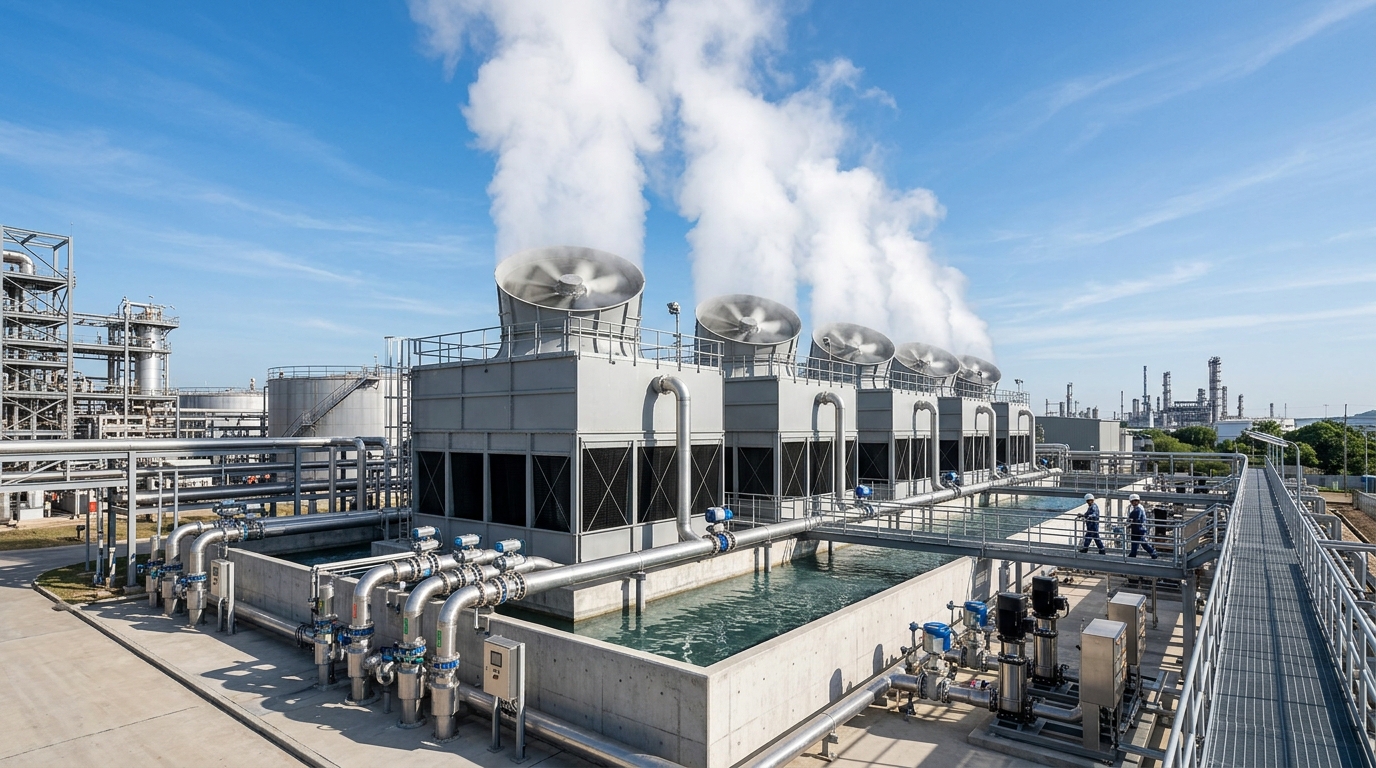
Cooling towers remove excess heat through evaporation – essential in industries like power generation, chemicals, textile dyeing, and HVAC. Because evaporation continually concentrates minerals and microbial growth, proper water treatment is vital to maintain heat exchange efficiency and protect system integrity.
MaxV® cooling tower programs cater to:
Prevents calcium carbonate, calcium sulfate, and silica scaling on condenser tubes, allowing higher Cycles of Concentration (COC) to save water.
Rapid-acting broad spectrum microbiological control eradicating algae, fungi, bacteria, and Legionella in cooling tower water loops.
Long-lasting residual biocides penetrating protective bio-slimes and sessile bacterial colonies resistant to conventional oxidizers.
Penetrates and breaks down stubborn bio-slime deposits, suspending dead organic matter and suspended solids for easy system purging.
Anodic and cathodic corrosion inhibitors forming a molecular protective film on carbon steel, copper, and yellow metal cooling components.
Stabilizes water alkalinity to maintain cooling water strictly within the Langelier Saturation Index (LSI) safe operating window.
High-performance polymeric and phosphonocarboxylate scale inhibitors engineered to protect polyamide, thin-film composite (TFC), and Murugappa RO/NF membranes against mineral crystallization, high reactive silica fouling, and metal oxide scaling.
| Product Name | Chemistry & Target Scales | Key Performance Features |
|---|---|---|
| MaxV® 9011 | Broad-Spectrum RO Antiscalant Organo-phosphonate & carboxylate copolymer blend |
High-efficiency threshold scale inhibitor controlling Calcium Carbonate (CaCO₃, LSI up to +2.6), Calcium Sulfate (CaSO₄), Barium Sulfate (BaSO₄), and Strontium Sulfate. Low continuous dosage (2–5 ppm) minimizes operational OPEX. |
| MaxV® 9014 | High-Silica & Heavy Metal RO Antiscalant Advanced acrylic-terpolymer & phosphonocarboxylate matrix |
Specifically engineered for high reactive & colloidal silica (SiO₂ up to 250–300 mg/L), iron, and manganese fouling. Prevents irreversible amorphous silica polymerization on membrane pores, extending runtime between CIP cleanings by 300%. |
| MaxV® 9015 | High-Recovery & ZLD-Grade RO Antiscalant Multi-polymer high-ionic-strength scale inhibitor & dispersant |
Designed for high-recovery (> 85–90%) secondary/tertiary RO stages, high-TDS industrial wastewater, and Zero Liquid Discharge (ZLD) concentrators. Operates under extreme super-saturation (LSI up to +2.8 to +3.0) and high sulfate/chloride stress. |
Maintains active threshold anti-precipitation across pH 5.0 to 9.0 without acid dosing requirements.
Fully compatible with polyamide, cellulose acetate, and TFC membranes from all major global manufacturers.
Engineered for accurate continuous metering at 2 to 6 ppm, lowering chemical handling and running costs.
Every MaxV® RO chemical program is backed by free raw water chemistry projection modeling:
Zero Liquid Discharge (ZLD) chemicals are crucial in industrial water treatment, ensuring no liquid waste is discharged and promoting maximum water reuse while minimizing environmental impact.
Effluent Treatment Plant (ETP) removes large suspended solids, colloidal matter, and heavy contaminants using high-performance coagulants and flocculants.
UF filters out fine sub-micron particles, colloidal silica, and high molecular weight organic matter using specialized membrane care formulations.
RO removes dissolved salts, silica, and heavy metal ions, producing ultra-pure water for reuse back in plant boilers and cooling towers.
MEE concentrates remaining RO brine reject by evaporating water in multiple stages, leaving dry crystallized salt and 100% water recovery.
Serving textile processing, thermal power generation, chemical synthesis, sugar, paper, and manufacturing facilities across India.
Broad-spectrum threshold inhibitors preventing mineral crystallization on RO membranes and boiler tubes.
Silicone and non-silicone defoamers for rapid foam knockdown in ETP aeration basins, cooling towers, and evaporators.
Oxidising and non-oxidising biocides preventing bacterial proliferation, algae blooms, and microbial fouling.
Specialized bacterial and enzymatic consortia enhancing biological digestion of COD, BOD, and refractory organics in ETPs.
Acidic and alkaline CIP membrane descalers and boiler offline cleaners that dissolve tenacious mineral scale safely.
Primary coagulants (PAC, inorganic & organic blends) that destabilize colloidal charges for rapid primary settling.
Volatile amine chemistries neutralizing carbonic acid in steam return lines, preventing pipe grooving and leaks.
Synergistic phosphate, molybdate, and polymeric blends that protect multi-metal water distribution networks.
High-molecular-weight cationic, anionic, and non-ionic polyelectrolytes for sludge dewatering and clarification.
Specialized chemical neutralizers that eradicate hydrogen sulfide (H2S), mercaptans, and anaerobic wastewater odors.
Sulfite, DEHA, and tannin-based oxygen scavengers for rapid feed-water de-aeration down to zero ppb.
Precision neutralizers and alkaline boosters designed for boiler feedwater, RO permeate re-mineralization, and ETP effluent.